Project Overview
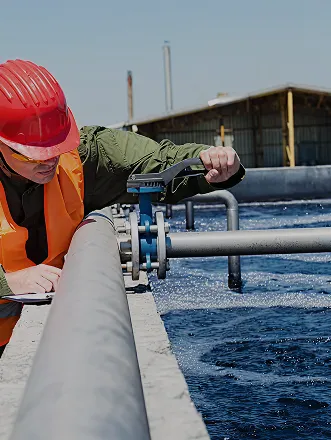
This project is a 50 T/H reclaimed water reuse equipment project for Luli Wood Industry, designed to support water recycling and reuse through filtration, ultrafiltration, reverse osmosis, and concentrate water collection.
The system adopts a combined process including quartz sand filtration, raw water storage, heat exchange, bag/self-cleaning filtration, ultrafiltration, intermediate water storage, precision filtration, reverse osmosis, and desalinated water storage. A chemical cleaning system is also configured for RO system maintenance.
This project provides a practical reference for industrial users requiring reclaimed water reuse, membrane treatment, and water resource recycling in production facilities.
Process Introduction
1. Front-End Filtration and Raw Water Storage
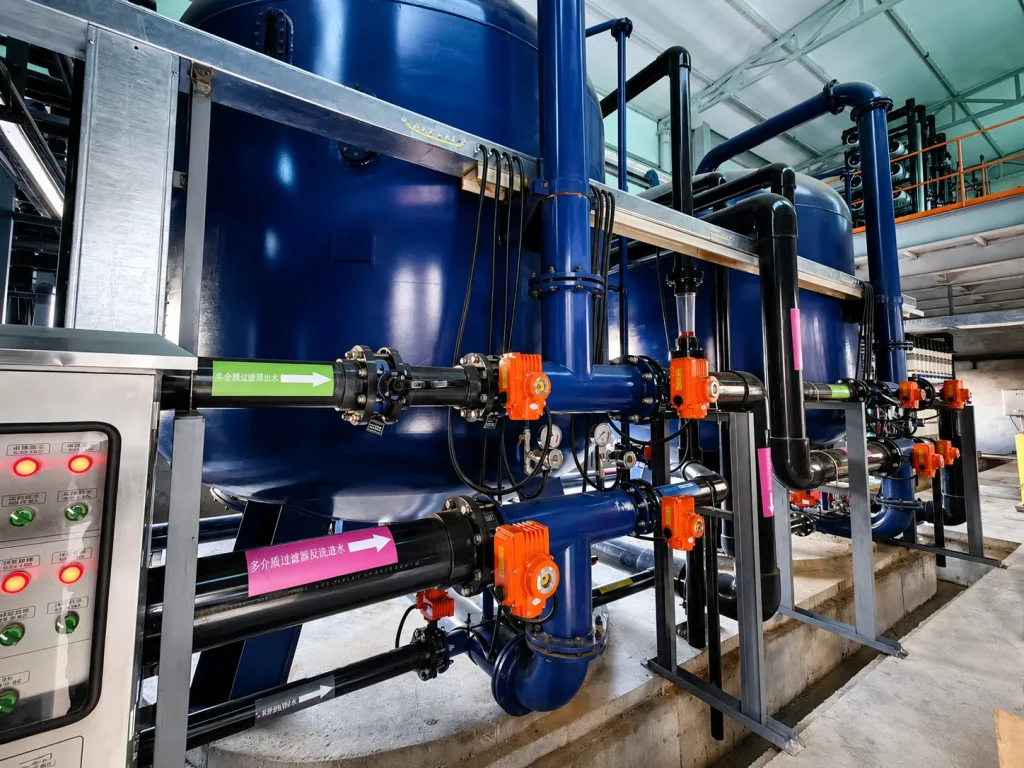
The incoming water first passes through a quartz sand filter and then enters the raw water tank. This stage is used as the front-end filtration section to reduce suspended impurities before the downstream membrane treatment process.
2. Ultrafiltration Pretreatment
Water from the raw water tank is delivered by the raw water pump and passes through a heat exchanger, then enters a bag/self-cleaning filtration unit and the ultrafiltration system.
The ultrafiltration section helps improve water clarity and reduce particulate load before reverse osmosis treatment, supporting more stable membrane operation.
3. Reverse Osmosis Treatment
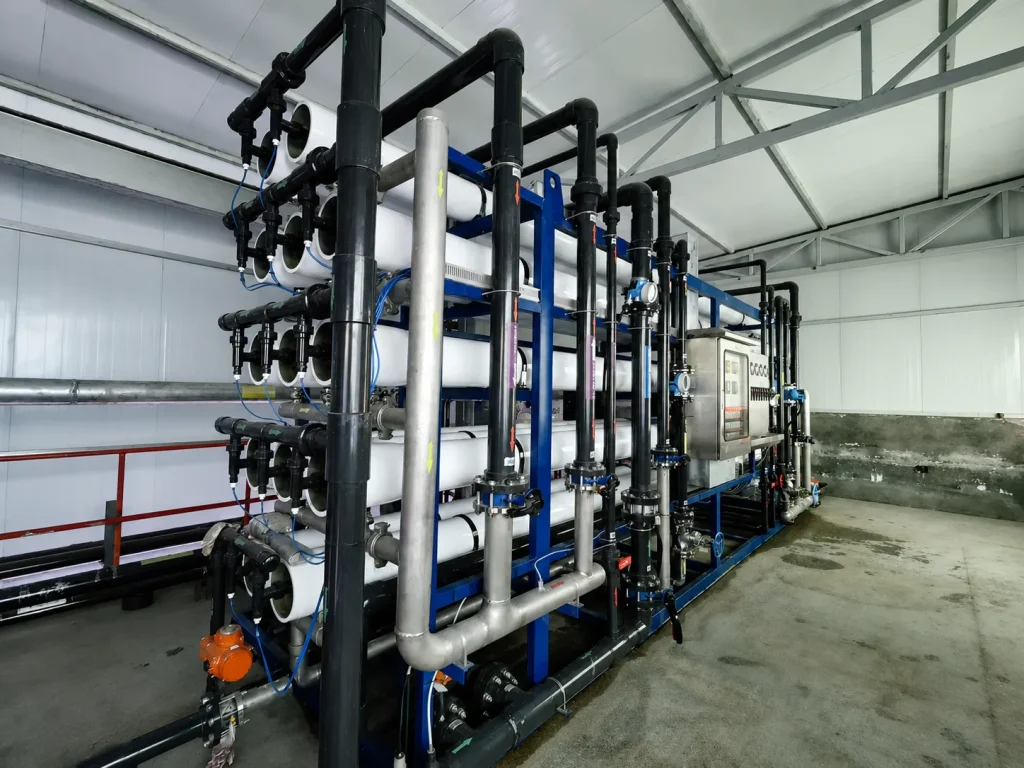
After ultrafiltration, the water enters the intermediate water tank, then passes through an intermediate precision filter before entering the reverse osmosis unit.
The RO system is configured with a concentrate water recovery system, helping improve water resource utilization within the reclaimed water reuse process. Treated water then enters the desalinated water tank for further use.
4. Chemical Cleaning Process
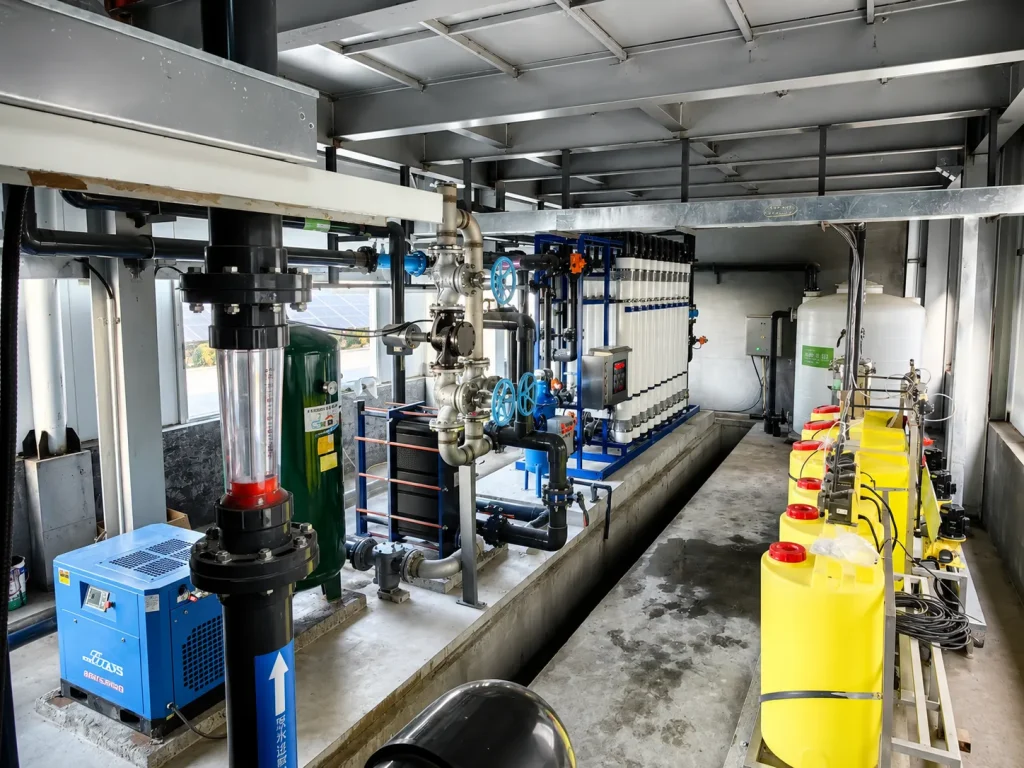
The system includes a chemical cleaning process for RO maintenance:
Cleaning agent → chemical cleaning tank → chemical cleaning pump → cleaning filter → RO unit
This configuration supports routine maintenance of the reverse osmosis system when cleaning is required.
5. Wastewater and Concentrate Collection
According to the provided process, wastewater and concentrate streams are collected as follows:
- Quartz sand filter backwash drainage and tank drainage are discharged into the concentrate water tank.
- Ultrafiltration backwash water and RO concentrate water are discharged into the concentrate water tank.
This arrangement helps collect backwash and concentrate streams in a centralized way for subsequent handling.
System Features
1. 50 T/H Reclaimed Water Treatment Capacity
The system is designed for a 50 T/H reclaimed water reuse project, supporting industrial water recycling requirements.
2. Multi-Stage Filtration Process
Quartz sand filtration, bag/self-cleaning filtration, ultrafiltration, and precision filtration are combined to protect downstream RO membrane operation.
3. UF + RO Membrane Treatment
The system uses ultrafiltration as pretreatment and reverse osmosis for deeper desalination and water quality improvement.
4. Concentrate Water Recovery Configuration
The RO section includes a concentrate recovery system, supporting more efficient water resource utilization.
5. Chemical Cleaning Support
A dedicated chemical cleaning process is configured for RO unit maintenance, helping support long-term membrane system management.
6. Centralized Wastewater Collection
Backwash water, tank drainage, UF backwash water, and RO concentrate are collected into the concentrate water tank for centralized handling.
Project Value
This case demonstrates a practical reclaimed water reuse process for industrial applications. By combining pretreatment, ultrafiltration, reverse osmosis, and concentrate collection, the system supports water recycling, membrane protection, and improved water resource utilization.
For industrial customers, reclaimed water reuse equipment can help reduce freshwater demand, support internal water circulation, and improve wastewater management when properly configured according to water quality and reuse requirements.
Conclusion
The Luli Wood Industry 50 T/H Reclaimed Water Reuse Equipment Project uses a process combining quartz sand filtration, ultrafiltration, reverse osmosis, concentrate recovery, chemical cleaning, and centralized concentrate collection.
This project provides a useful reference for industrial customers seeking reclaimed water reuse equipment and membrane-based water recycling solutions.




 June 24, 2026